Industrial Adhesives & Sealants Manufacturer
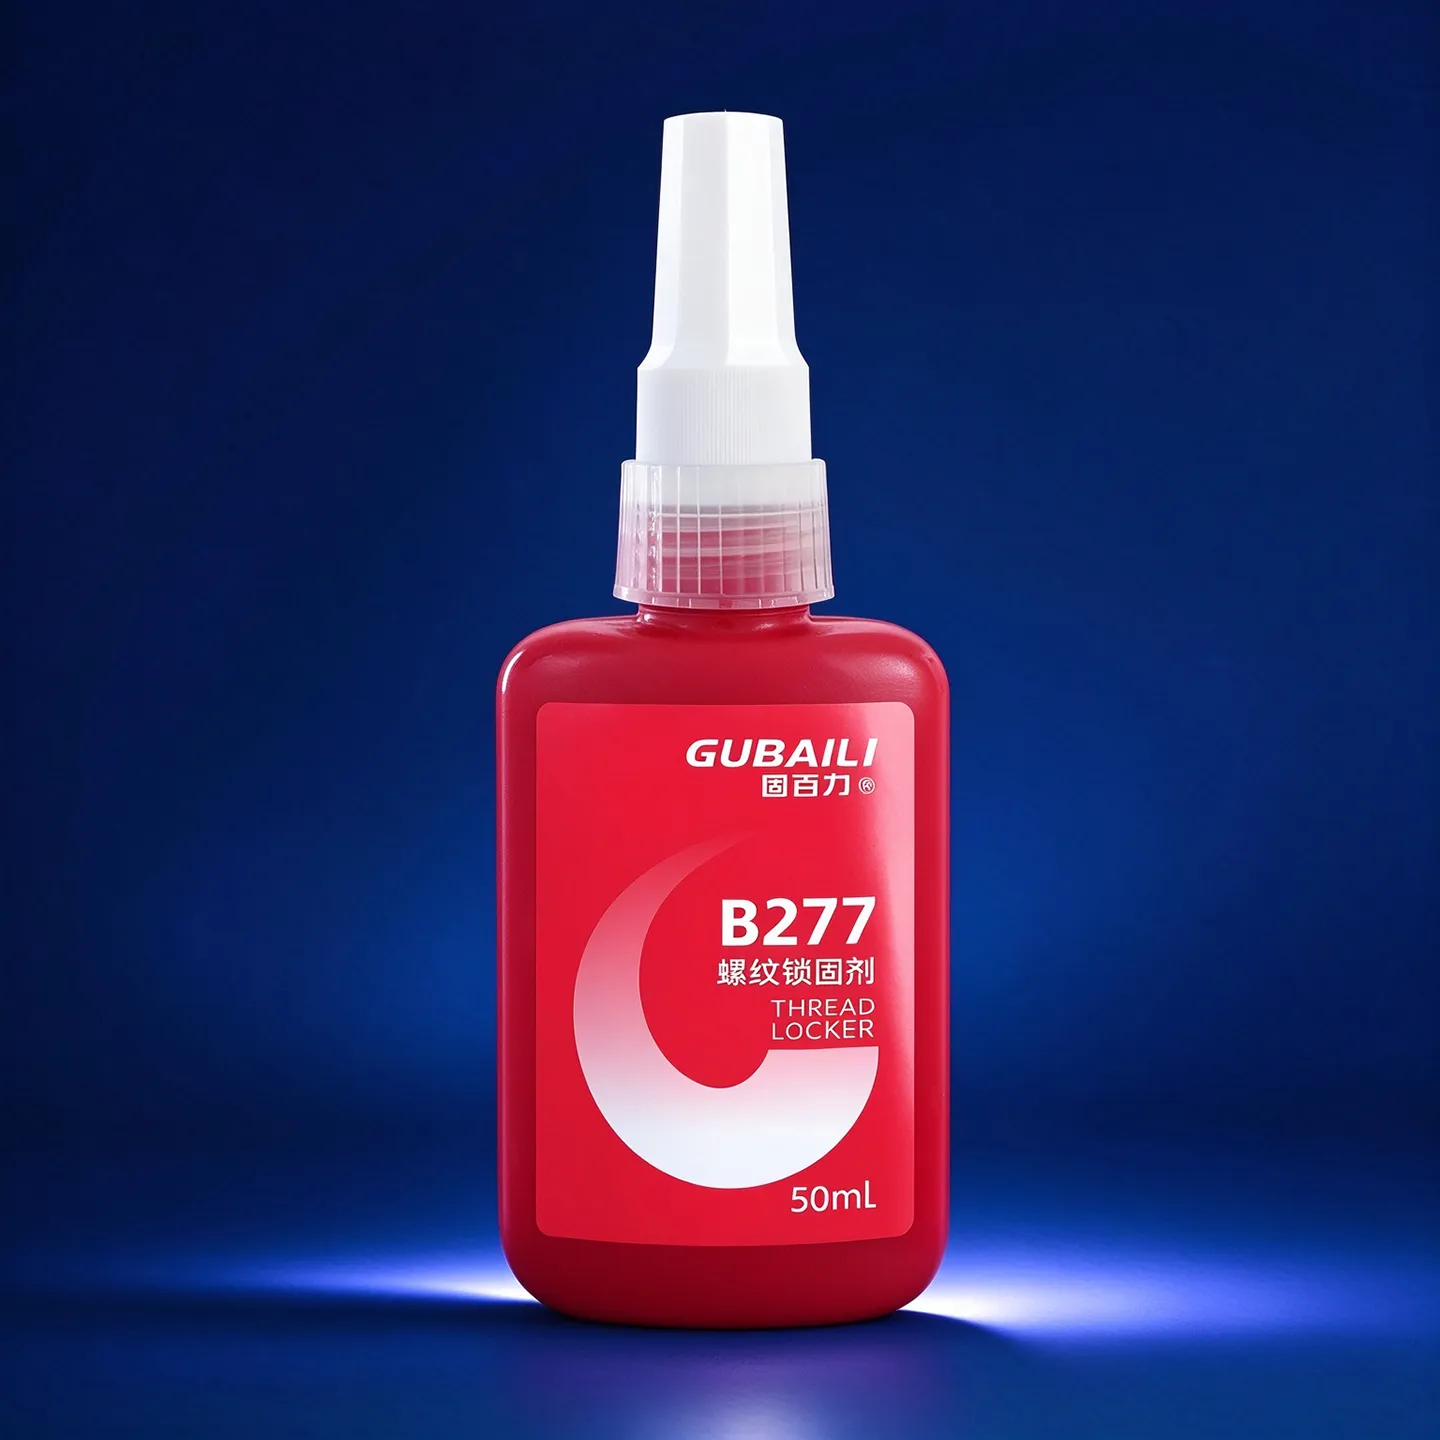
GUBAILI B277 red high-strength threadlocker: high viscosity 7000 cP, for permanent locking and sealing of large bolts and studs up to M80. Service temperature -55 to 150°C, heat required for disassembly. 50 ml/250 ml available.
High bond strength for structural joints under heavy loads.
High consistency that resists run-off, ideal for filling large gaps.
Stable performance over a wide temperature range.
Effectively prevents thread loosening.
| Parameter | Specification / Value |
|---|---|
| Viscosity | 7000 cP |
| Color | Red |
| Thixotropic | No |
| Thread Size | M80 and below |
| Initial Set Time | 45 min |
| Breakaway Torque | 32 N·m (280 lb.in) |
| Average Removal Torque | 32 N·m (280 lb.in) |
| Temperature Range | -55°C ~ 150°C (-65°F ~ 300°F) |
| Strength | High strength, permanent locking, localized heat required for disassembly |
| Packaging | 50 ml / 250 ml |
Product Overview
GUBAILI B277 is a red anaerobic threadlocker with high viscosity and high strength. It is a permanent threadlocking grade that requires localized heating for disassembly. Designed specifically for large threaded fasteners, it cures in confined thread clearances to permanently lock and seal bolts and studs, resisting loosening from equipment vibration and impact. It suits high-strength locking of large threads in heavy machinery and large equipment.
Industries
For permanent locking and sealing of large bolts and studs up to M80. Widely used for anti-loosening of large threaded assemblies in heavy machinery, wind power equipment, shipbuilding and large reducers.
Instructions
1. Clean oil, dust and rust from the threads and ensure the surfaces are clean and dry;
2. Apply adhesive evenly at the thread engagement area and assemble/tighten into position;
3. Initial set takes 45 minutes at room temperature; full cure strength is reached after 24 hours;
4. If disassembly is required, heat the threaded area locally before removing.
Precautions
1. Anaerobic adhesive—cures only in confined metal gaps and will not cure in open air;
2. High-viscosity formula resists run-off on large vertical threads;
3. Work in a ventilated area and avoid contact with skin and eyes;
4. Not suitable for plastic, rubber or other non-metallic threads;
5. Store in a cool, dark place away from heat.
Threads should be degreased, derusted and dry. For blind holes, control the amount of adhesive so it is not forced to the bottom and trapped as a hydraulic lock; for through holes, apply adhesive around the full circumference of the external thread.
Apply adhesive to the engagement area, not the bolt tip, and tighten to torque specification after assembly. Do not let adhesive enter bearings, oil passages or moving joints.
Anaerobic adhesives cure when isolated from air and in contact with metal. Initial set typically takes 10–30 minutes and final strength about 24 hours; low temperatures extend these times.
Low- and medium-strength joints can be disassembled with tools. For high-strength joints, heat to about 250°C and disassemble while hot to avoid twisting off the bolt.
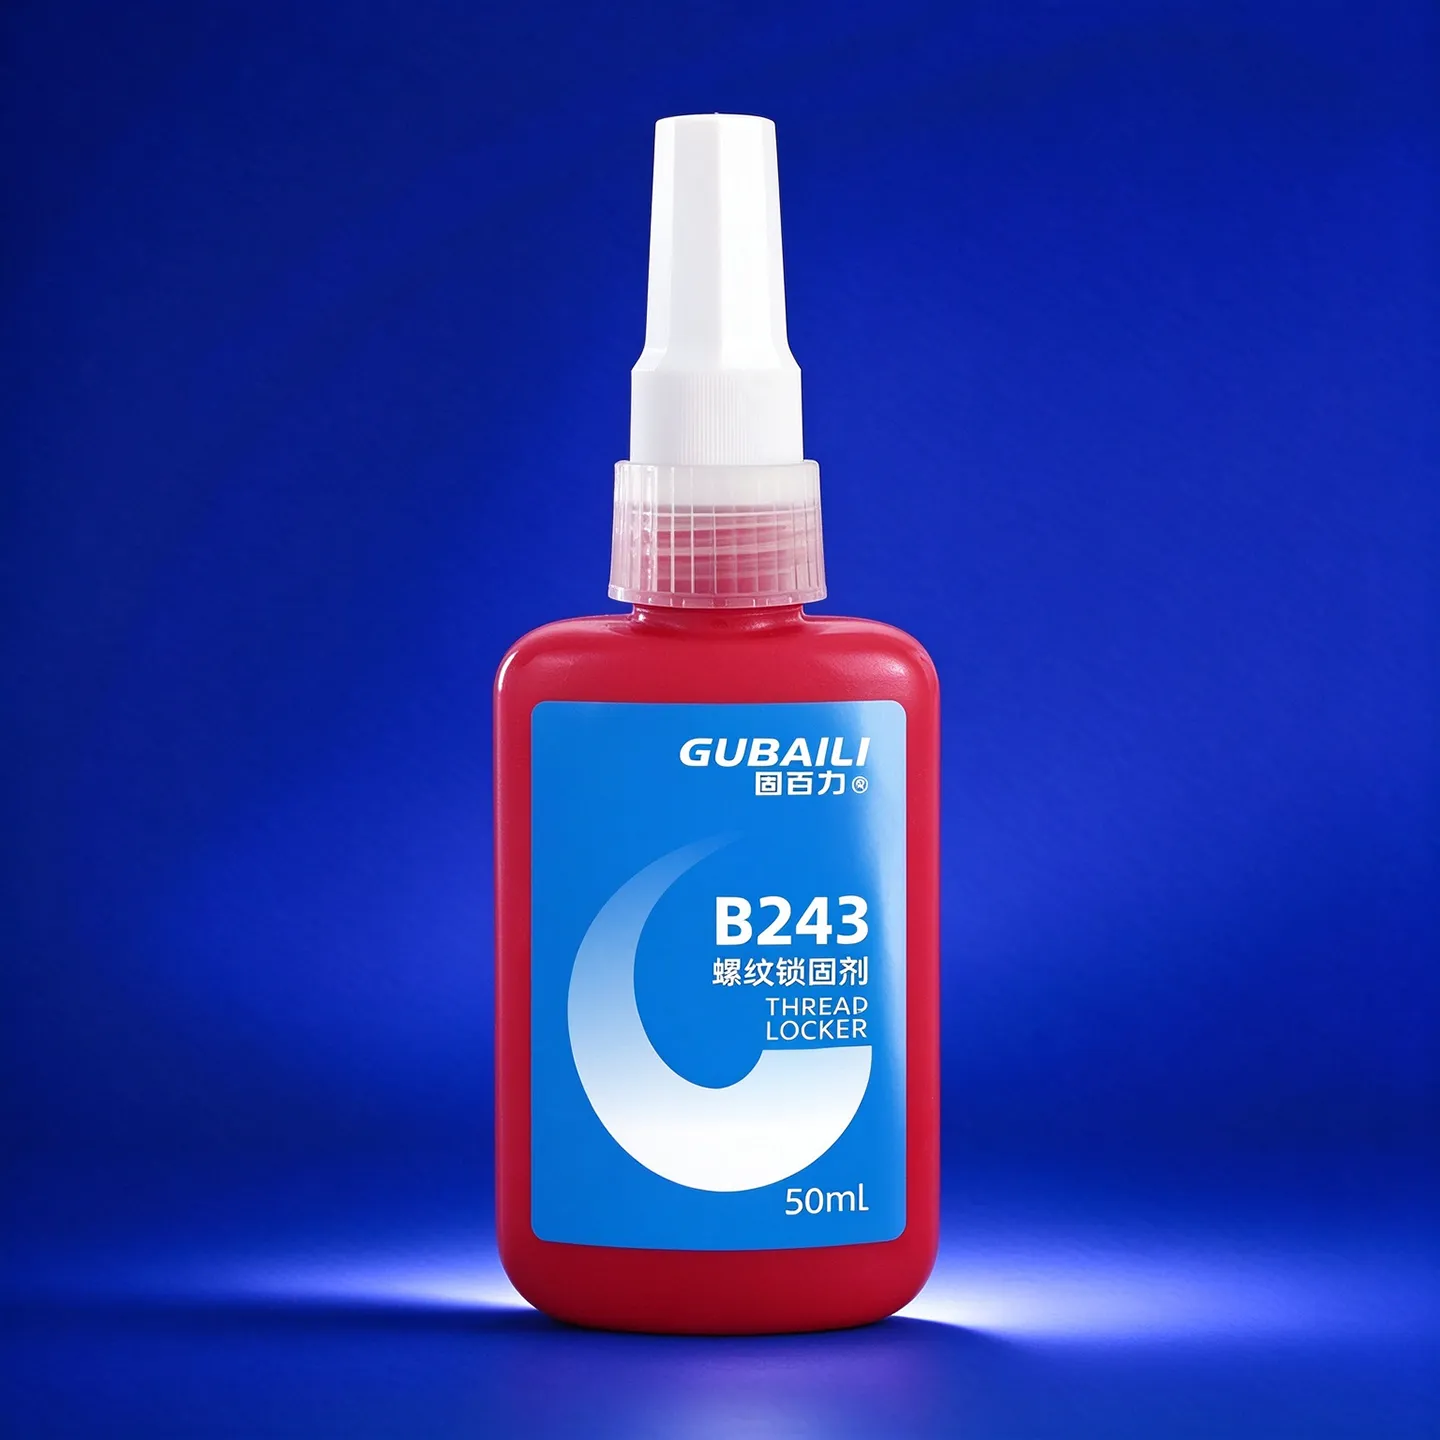
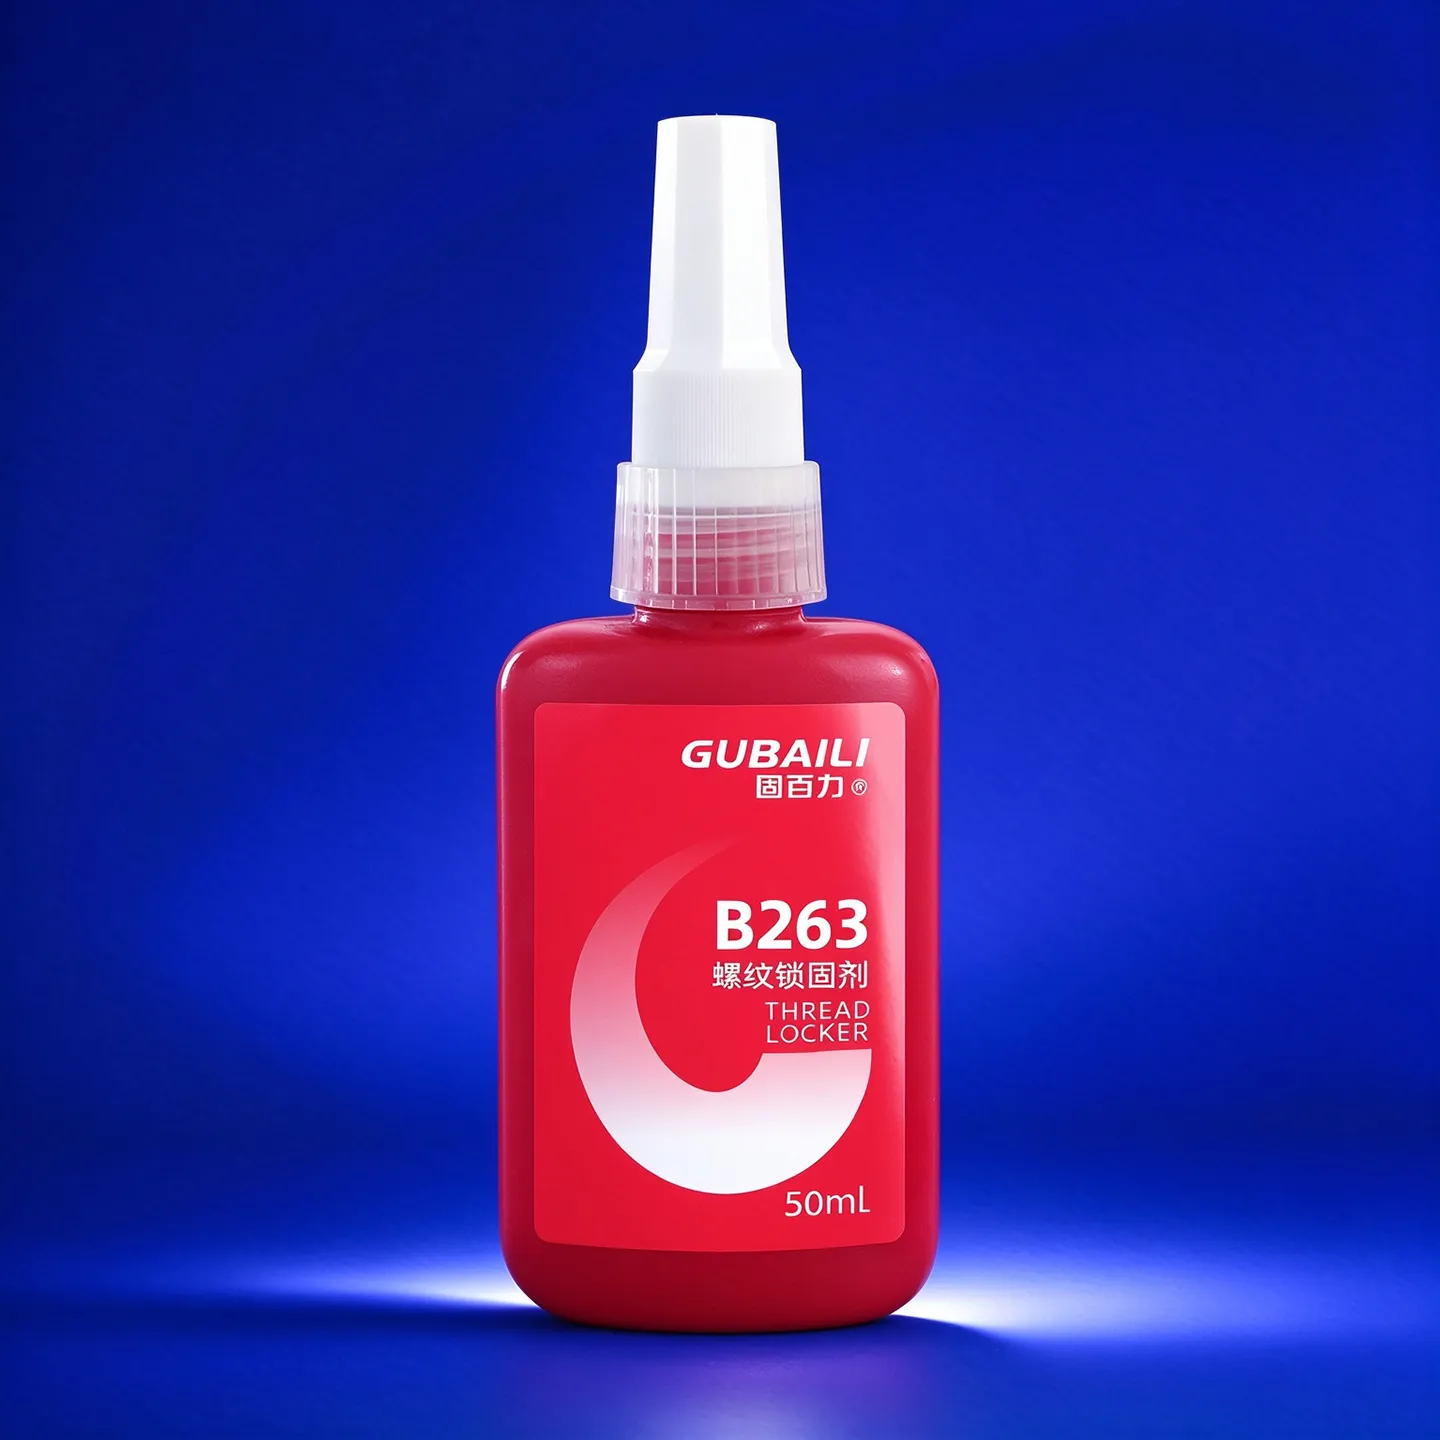
For small screws that are frequently adjusted or serviced, choose low-strength B222, removable with hand tools; for general machinery assembly, choose medium-strength B243; for heavy-duty joints that are rarely disassembled, choose high-strength B263.
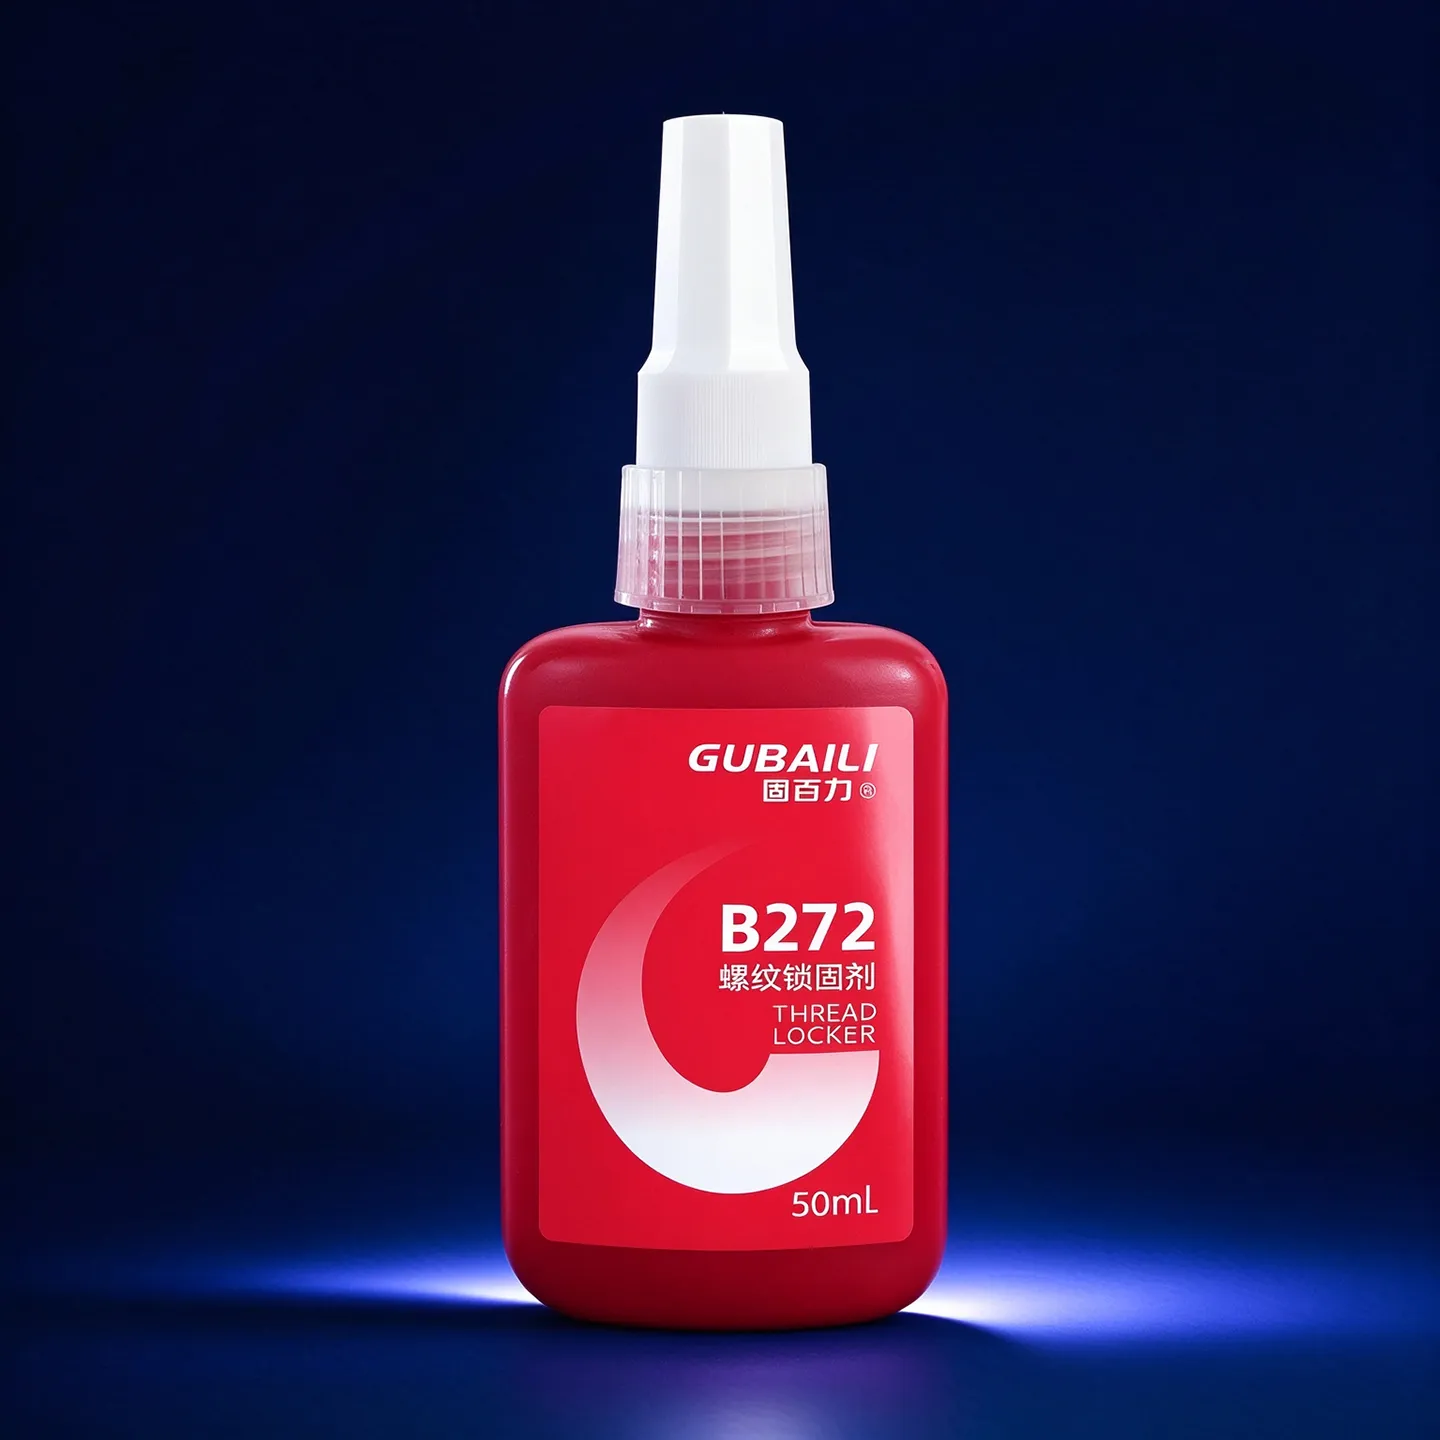
For high-temperature applications choose B272; for bolts above M25 choose B277; for reinforcing already-assembled bolts choose penetrating grade B290. The higher the strength, the more disassembly depends on heat or special tools.
For bolts above M25, apply adhesive over the full engagement length rather than only at the end.
Large bolts require high tightening torque; confirm the adhesive film has not been scraped off before assembly, and tighten to specification.
We customise formulations by substrate, viscosity, cure speed and media resistance, and provide sample testing and technical selection support.
Tell us about your application and our engineers will provide product recommendations, sample dispatch and technical support within 48 hours.