Industrial Adhesives & Sealants Manufacturer
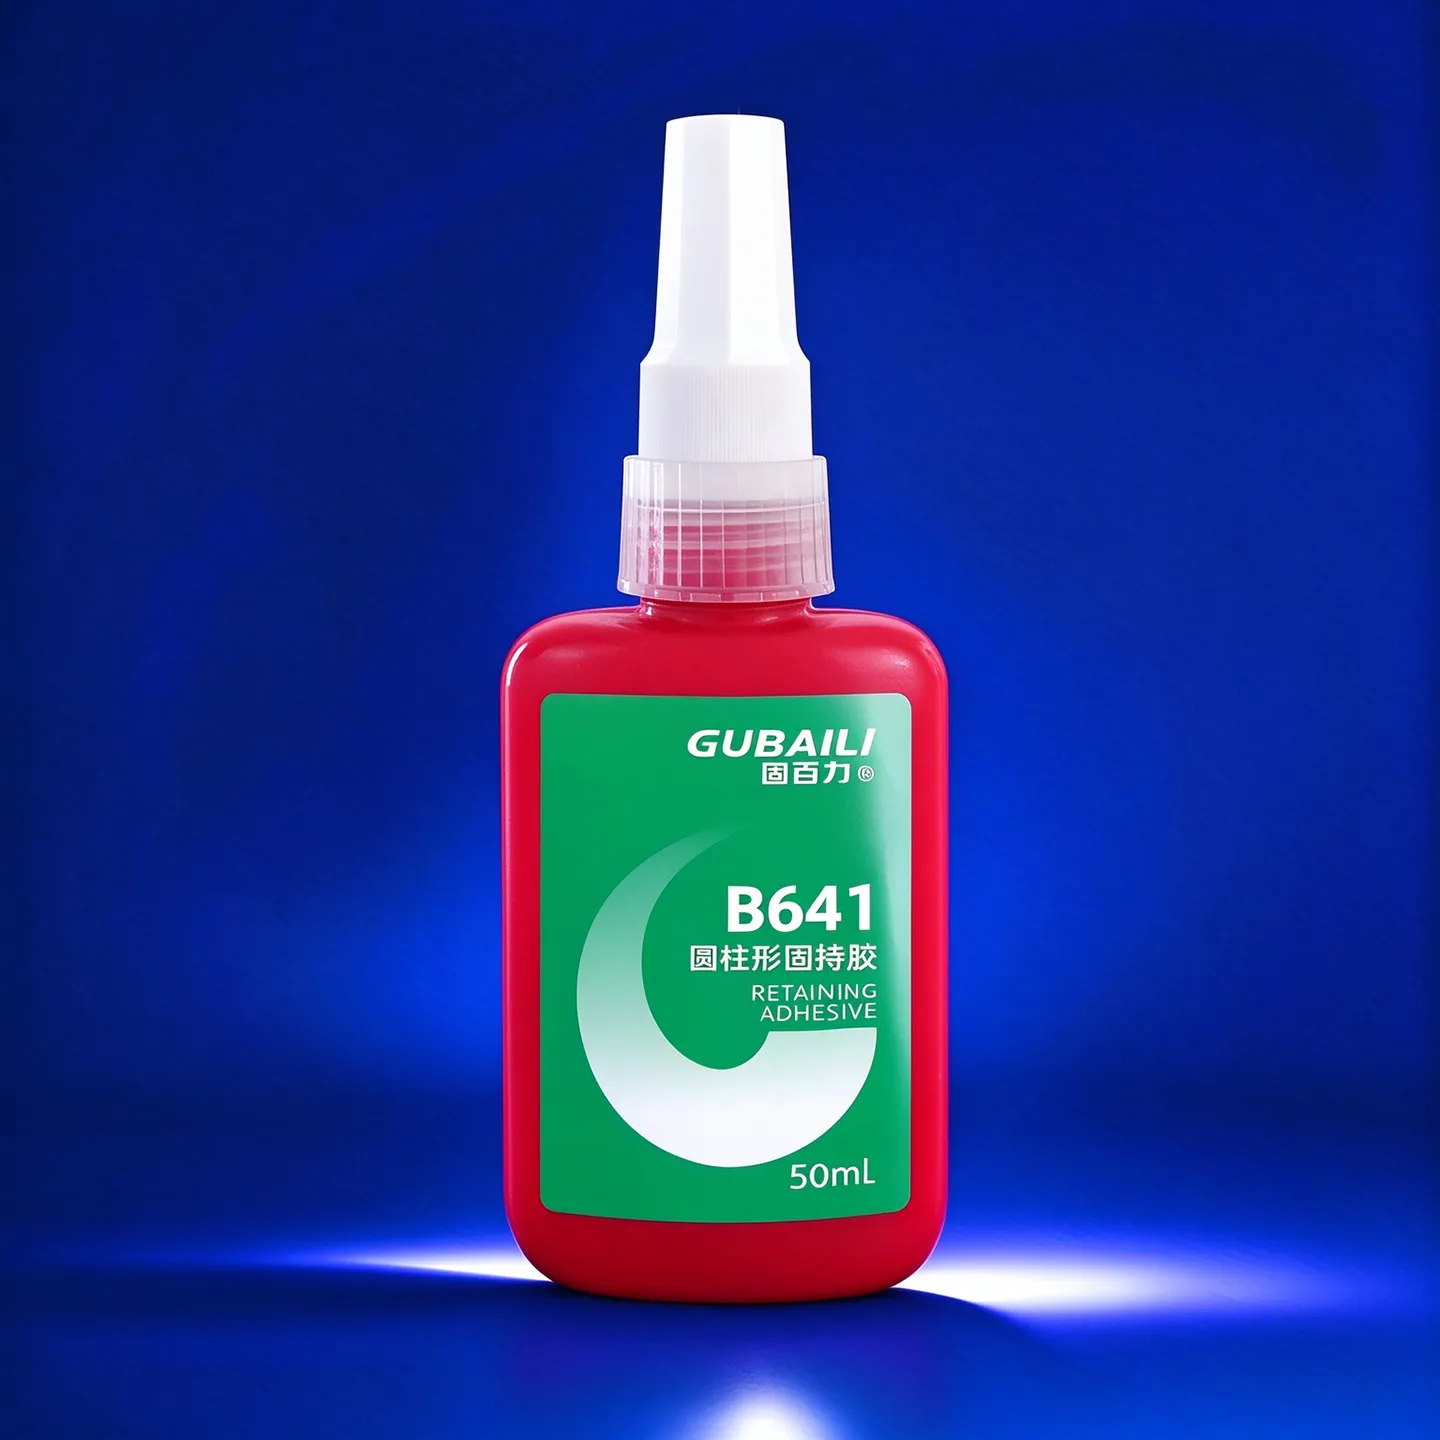
GUBAILI B641 yellow retaining compound: viscosity 600 cP, medium strength and removable, suitable for clearances within 0.2 mm, for bearings requiring later maintenance and disassembly. Service temperature -54 to 150°C. 50 ml/250 ml available.
Moderate strength balancing reliability with easy disassembly.
Excellent flow and penetration for bonding tight gaps.
Non-sagging at rest, flows under shear for easy application.
Removable for easy maintenance.
| Parameter | Specification / Value |
|---|---|
| Viscosity | 600 cP |
| Color | Yellow |
| Thixotropic | No |
| Radial Clearance | < 0.006 in. / 0.2 mm |
| Initial Set Time | 20 min |
| Compressive Shear Strength (Steel-to-Steel) | 940 psi (6.5 N/mm²) |
| Temperature Range | -54°C ~ 150°C (-65°F ~ 300°F) |
| Key Properties | Medium strength, low viscosity, removable |
| Packaging | 50 ml / 250 ml |
Product Overview
GUBAILI B641 is a yellow, low-viscosity anaerobic retaining compound with a medium-strength formula that allows later disassembly, with no thixotropy. This one-component anaerobic adhesive cures only in confined metal gaps isolated from air and suits cylindrical fit assemblies with radial clearance below 0.2 mm. After curing, it fills the fine clearance between shaft and bore, improving the assembly strength of bearings, bushings and other cylindrical parts and suppressing loosening and fretting wear caused by operating vibration. Unlike permanent retaining compounds, its moderate bond strength allows disassembly with tools during maintenance, meeting the needs of assemblies that are repeatedly serviced. Its low viscosity and good flow fully wet narrow clearances, and the stable room-temperature cure reaches initial set in 20 minutes for production-line assembly.
Industries
Widely used for cylindrical components requiring later disassembly and maintenance in motors, transmission mechanisms and fixtures. Typical applications include retaining bearings in shafts or housings, for precision press fits with clearance within 0.2 mm.
Instructions
1. Clean oil, rust and dust from the shaft and bore mating surfaces and keep them dry;
2. Apply adhesive evenly to the mating surfaces and press the parts together quickly into position;
3. Initial set takes 20 minutes at room temperature; final cure strength is reached after 24 hours;
4. Keep radial clearance within 0.2 mm; excessive clearance reduces bond strength.
Precautions
1. Anaerobic adhesive cures only in oxygen-free confined metal gaps and will not cure when exposed to air;
2. This grade is removable and not suitable for applications requiring permanent locking or extremely high loads;
3. Work in a ventilated area, avoid contact with skin and eyes, and wear protective equipment;
4. Not suitable for retaining plastic, rubber or other non-metallic substrates;
5. Store sealed in a cool, dark place away from heat.
Degrease and derust both shaft and bore, and keep them dry. Apply adhesive evenly around the circumference of the mating surface, and rotate while pressing in to distribute the adhesive and expel air.
Use enough adhesive that a small bead squeezes out at the joint edge after assembly. Keep adhesive out of bearing races, oil holes and other moving parts, and let the assembly cure undisturbed per the process.
Standard grades suit general conditions; for long-term high temperature choose B620 or B648; for contact with oil or light oil contamination choose B638 or B648. Refer to the grade data sheet and actual testing for specific temperature ranges.
If the temperature limit is exceeded, switch to a structural adhesive or mechanical reinforcement—do not try to solve it by adding more adhesive.
For small clearances and fast press fits, choose low-viscosity B609; for general shaft-to-hub fits, choose B603; for worn or oversized clearances, choose B680 with greater gap-filling capability.
For assemblies requiring periodic maintenance or disassembly, choose B641; for high-temperature or oily environments, prefer B620, B638 and B648 respectively. Measure actual clearance and coaxiality before selection.
For shaft-to-hub fits that require periodic disassembly, such as frequently serviced pump shafts, rollers and bushings.
Use special tools or moderate heat during disassembly, and avoid hammering that damages the mating surfaces.
We customise formulations by substrate, viscosity, cure speed and media resistance, and provide sample testing and technical selection support.
Tell us about your application and our engineers will provide product recommendations, sample dispatch and technical support within 48 hours.