Industrial Adhesives & Sealants Manufacturer
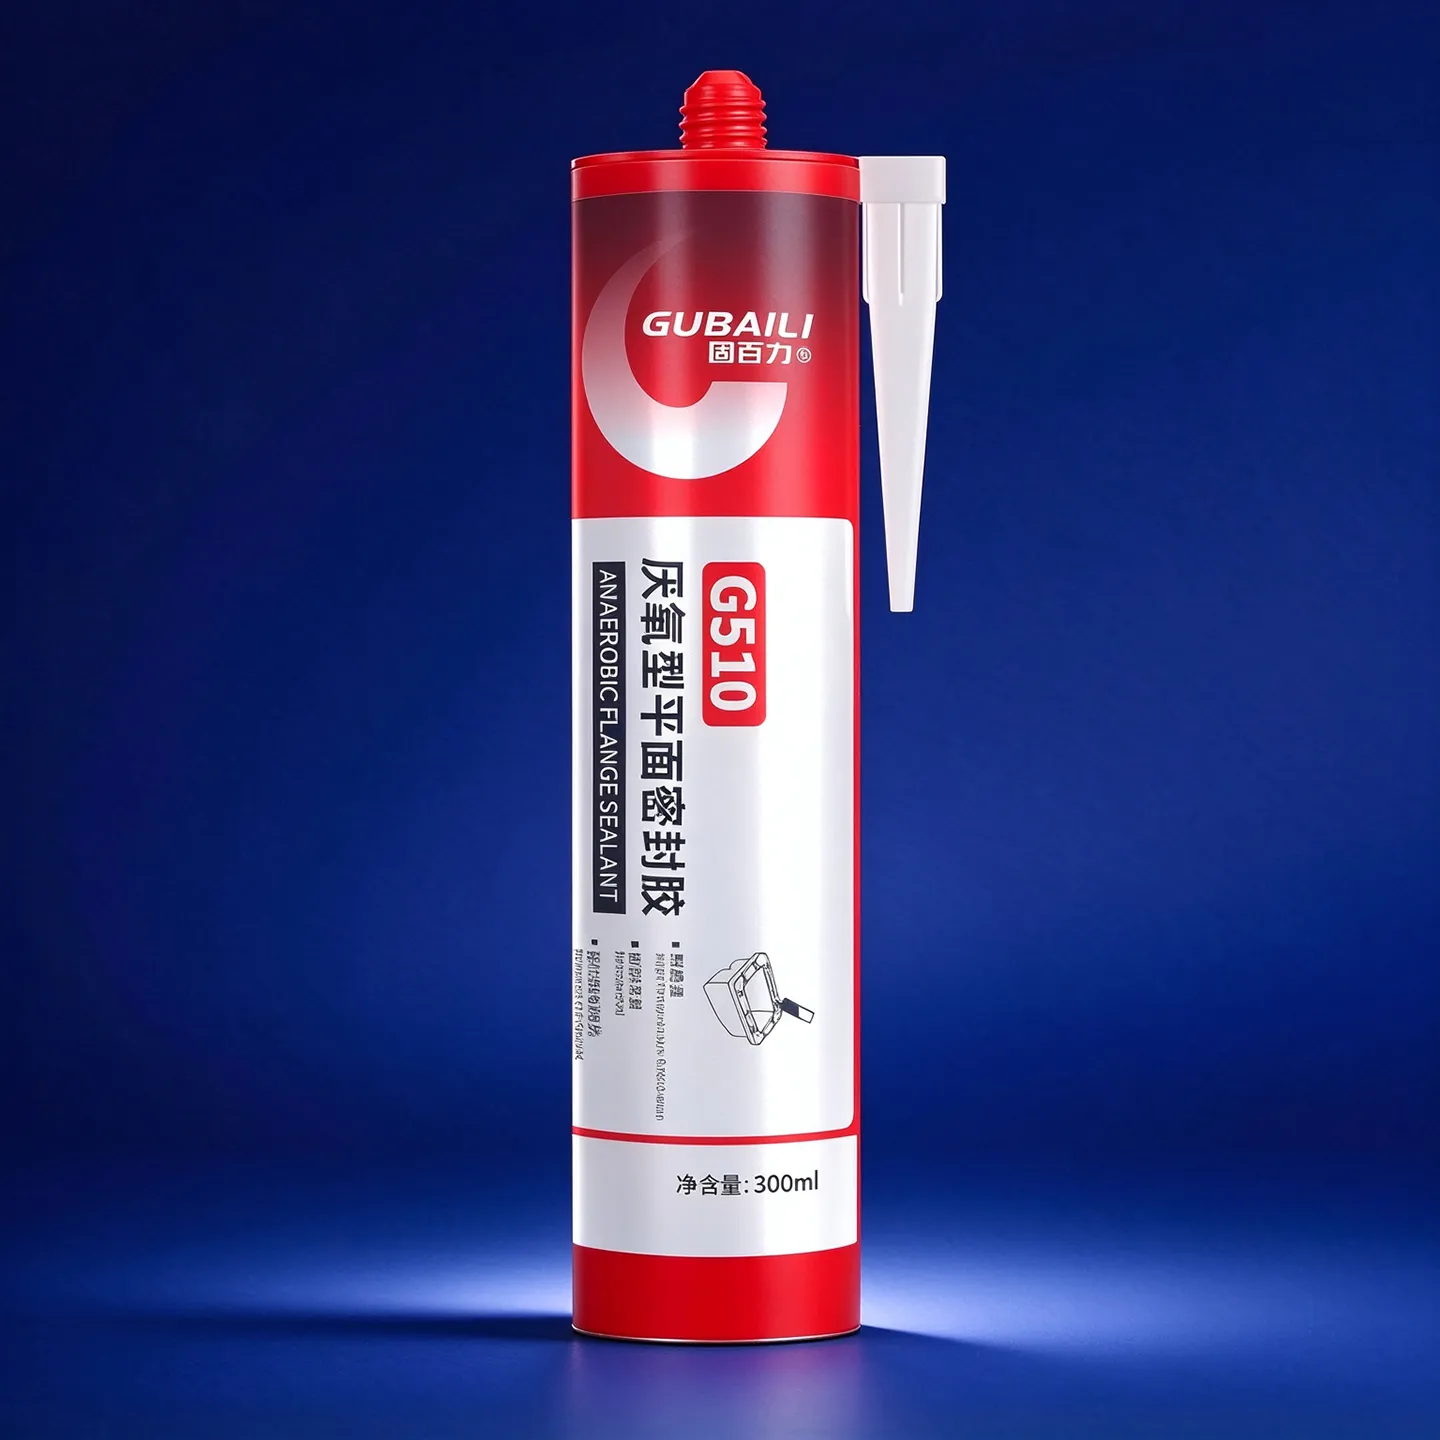
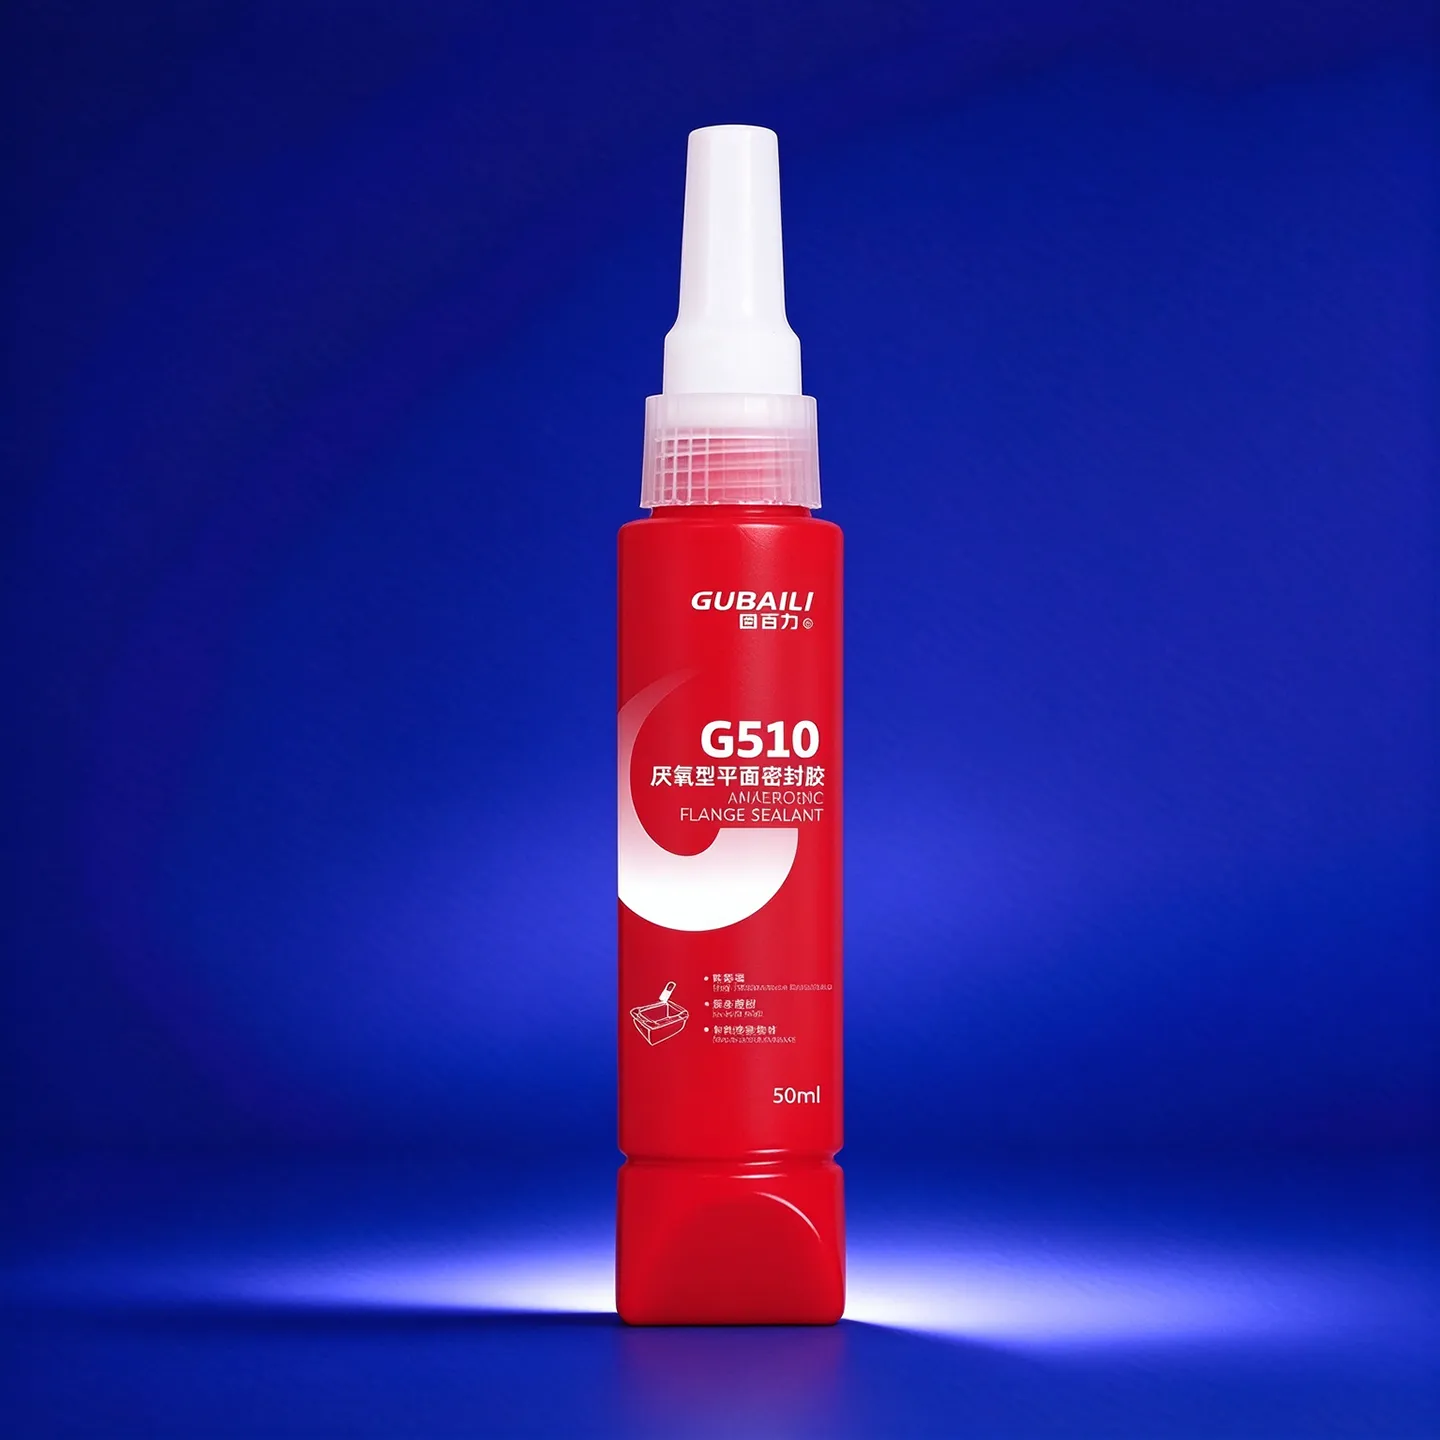
GUBAILI G510 one-component anaerobic sealant: pink gel, high-temperature resistance up to 204°C, maximum gap fill 0.25 mm, for rigid steel and aluminum flanges, gearbox and motor housings, NSF P1 certified. 50 ml/300 ml packs.
Non-sagging at rest, flows under shear for easy application.
Resists acids, alkalis, solvents and other media.
Forms a tight seal against gas and liquid leakage.
Universal compatibility with a wide range of substrates.
| Parameter | Specification / Value |
|---|---|
| Product Type | Gasket sealant |
| Chemistry | Methyl methacrylate |
| Cure System | Acrylate anaerobic curing |
| Components | One-component |
| Form | Gel |
| Color | Pink |
| Strength Level | Medium strength |
| Viscosity (20 RPM) | 90000 mPa·s (cP) |
| Maximum Gap Fill | 0.25 mm (0.01 in.) |
| Initial Set Time (Steel) | 25 minutes |
| Continuous Service Temperature | -55°C ~ 200°C |
| Storage Temperature | 8°C ~ 21°C |
| Features | Thixotropic, chemical resistant, high-temperature resistant, NSF P1 certified |
| Recommended Substrates | Steel, aluminum |
| Packaging | 50 ml / 300 ml |
Product Overview
GUBAILI G510 is a high-temperature formed-in-place anaerobic gasket sealant based on a one-component acrylate anaerobic system. The adhesive is a pink gel with excellent thixotropy that resists run-off after application, suitable for automated dispensing or manual application. It cures anaerobically by crosslinking in tightly fitted metal contact areas isolated from air, forming a low-pressure seal immediately after assembly and replacing conventional solid gaskets with an integrated flange-face seal. With a maximum temperature resistance of 204°C, it suits long-term high-temperature operation and fills flange gaps up to 0.25 mm, compensating for machining scratches and slight surface unevenness while improving the torque capacity of the assembled flange. It is NSF P1 certified and suitable for food machinery applications. The cured sealant resists chemicals, engine oil, machining fluids and some industrial media, and is designed for rigid steel and aluminum flanges.
Industries
Widely used in construction machinery, automotive drivetrains, motors and hydraulic pumps and valves. Typical applications include gearbox housings, motor housings, rigid flange sealing, interference-fit component sealing, and machined metal joints requiring long-term high-temperature and leak-free performance.
Instructions
1. Pre-treat the flange sealing surface, thoroughly removing oil, metal chips, old gasket residue and dust, and keep it dry and clean;
2. Apply a continuous, uniform bead along the sealing path to form a complete line without breaks; the thixotropic formula resists run-off on vertical surfaces;
3. Align the parts and tighten the bolts so the flange fits tightly; the confined gap triggers anaerobic curing;
4. Initial set on steel takes about 25 minutes at 25°C, after which the part can be moved; allow full cure before pressure service;
5. Wipe uncured squeeze-out with anhydrous ethanol or acetone; cured sealant can be disassembled by heat or mechanical means.
Precautions
1. Store strictly at 8-21°C in a cool place, away from heat and direct sunlight, to prevent premature failure;
2. Only suitable for tightly fitted rigid metal flanges; non-metallic substrates and wide-open gaps cannot exclude air and will not cure properly;
3. Work in a ventilated area and wear protective gloves to avoid contact with skin and eyes;
4. Do not use in continuous immersion in strong acids, alkalis or solvents;
5. Do not exceed a seal gap of 0.25 mm; excessive gaps cause poor curing and seal failure;
6. Keep away from children; this is an industrial adhesive and must not be ingested.
Degrease, derust and remove old sealant and burrs from the flange face, and keep it dry. Apply a continuous closed bead, keeping clear of the inside of bolt holes and leaving bolt passages open.
After assembly, tighten in stages in a diagonal sequence to the specified torque, avoiding squeezing the sealant out on one side and creating an interruption in the seal.
Anaerobic types suit medium-to-high temperature sealing of rigid structures, while silicone types cover a wider temperature range and remain flexible. For oil contact, select an oil-resistant grade based on the media. Refer to the data sheet for specific temperatures.
To disassemble, separate the flange first, then remove residual sealant with a scraper or dedicated cleaner without scratching the sealing face; leftover sealant will impair the next seal.
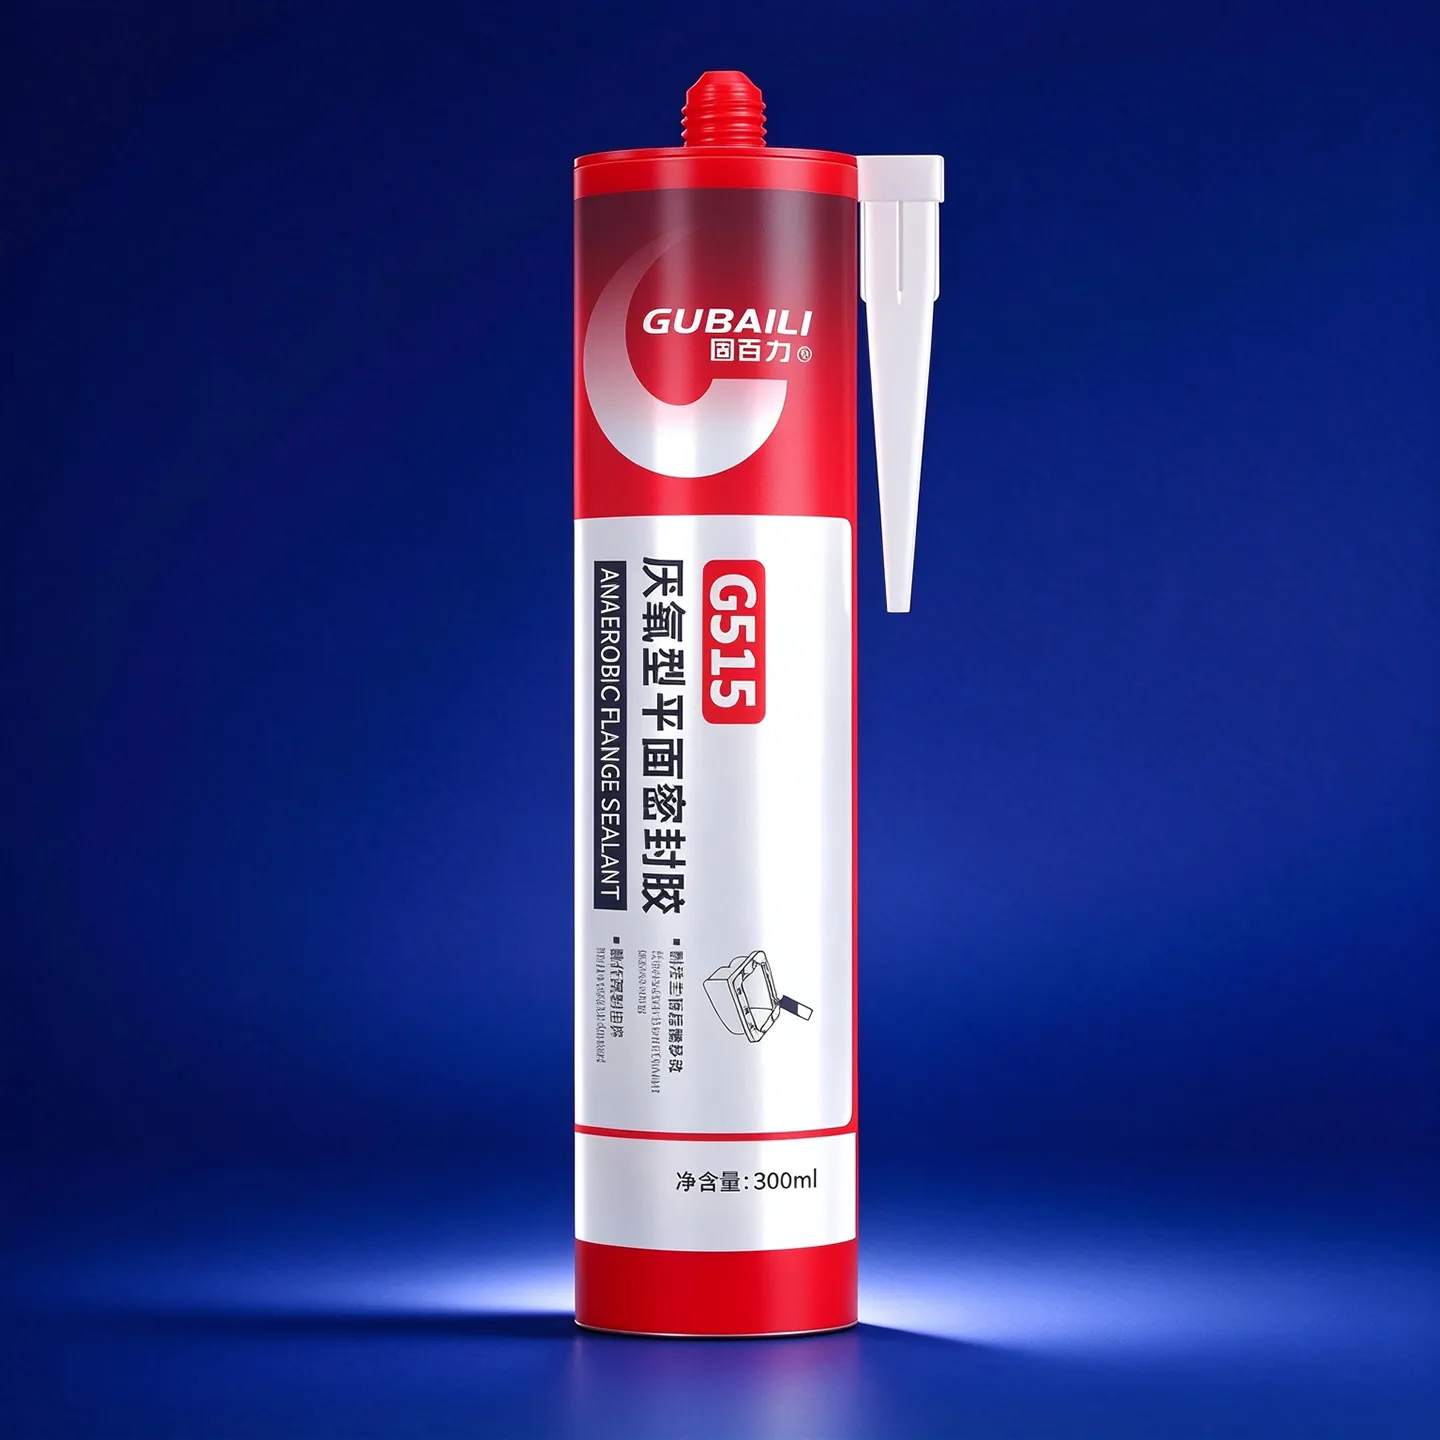
For rigid flanges requiring immediate pressure resistance and high temperature performance, prefer anaerobic types such as G510 and G515; for stamped sheet metal, uneven gaps or slightly distorted flanges, choose semi-flexible G518.
For high temperature or a wider temperature range, choose silicone types G596 and G598; for oil contact, prefer G5699; to replace conventional gaskets, choose G587.
For formed-in-place sealing of rigid flanges, pump bodies and high-temperature applications, forming an immediate seal.
Apply a continuous closed bead and tighten to specification to avoid interruptions in the seal line.
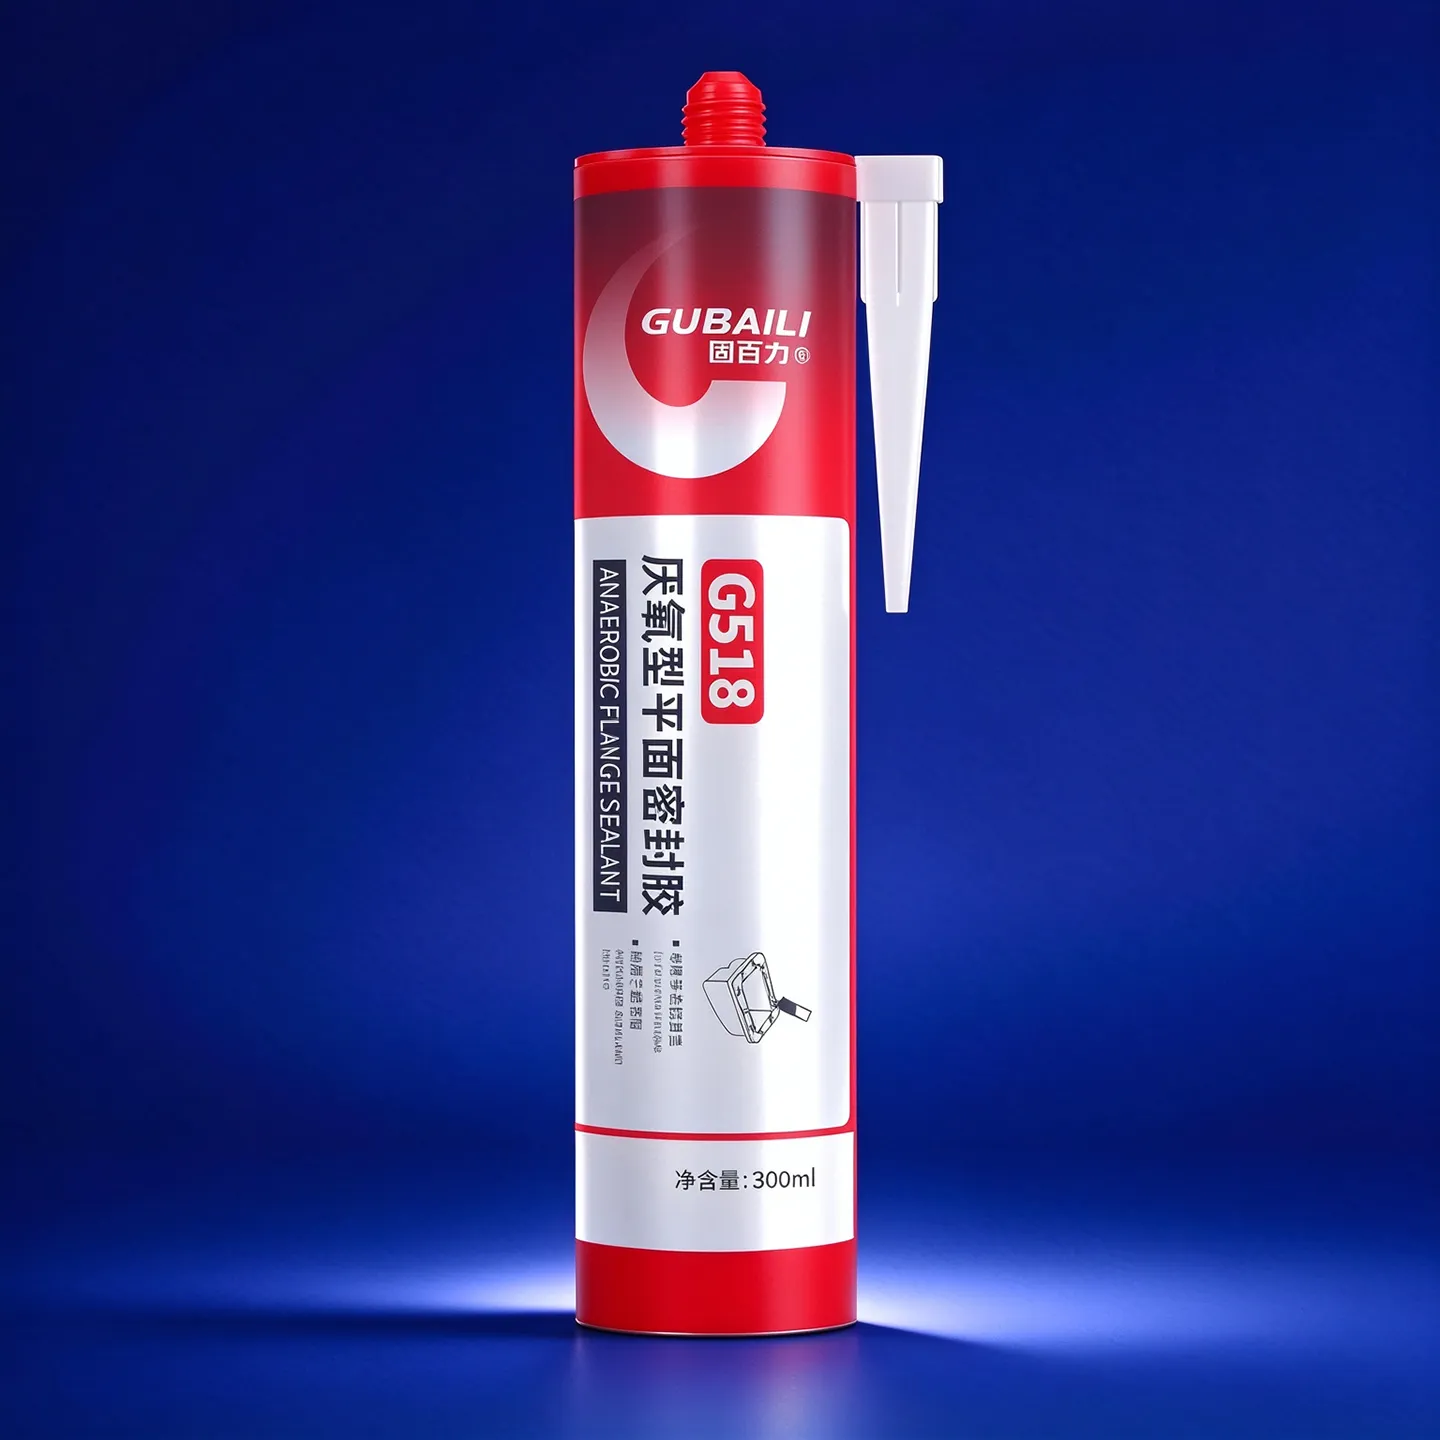
We customise formulations by substrate, viscosity, cure speed and media resistance, and provide sample testing and technical selection support.
Tell us about your application and our engineers will provide product recommendations, sample dispatch and technical support within 48 hours.